How to Choose the Right Powder Packaging Machine?
Choosing the right Powder Packaging Machine begins with the powder itself. Fine flour can drift and create dust. Granules may bridge inside a hopper. A blend with varied particle sizes can separate during feeding. These differences affect filling accuracy, line speed, and cleaning time. A machine that performs well with one product may struggle with another.
Before comparing models, define the details of your real operation. Note the powder’s flow behavior, bulk density, target pack weight, bag or pouch dimensions, and expected output. Ask suppliers to run trials using your product and packaging materials. Watch the fill settle. Check the seals. Record weight variation and changeover time. Small details matter: a narrow chute, static cling, or a difficult-to-reach corner can become a daily frustration. And brochures rarely show those moments.
A useful selection principle is simple: “Choose for the powder you actually run, not the powder in the brochure.” This is an original editorial line, not a verified quotation from a named industry expert. No source was provided to confirm an expert’s exact words, so attributing a quotation would risk misleading readers. A trustworthy evaluation should instead rely on documented trials, clear specifications, and service commitments. Consider dust control, cleaning access, spare-part availability, and operator training alongside purchase price. The best choice is not always the fastest machine. It is the one that delivers consistent packs under your actual production conditions. Some uncertainty remains until testing; that is worth admitting.
Assess Powder Flow Using Carr’s Index: 100 × (1 − Bulk/Tapped Density)
How to Choose the Right Powder Packaging Machine?
Carr’s Index estimates how much a powder consolidates during tapping: 100 × (1 − bulk density / tapped density). Measure both densities using the same sample and controlled conditions. For example, bulk density of 0.50 g/mL and tapped density of 0.625 g/mL produce an index of 20%. Small differences matter. Moisture, handling, and inconsistent tapping can shift the result.
Carr’s 1965 flowability scale places an index around 16–20% in the fair range and 26–31% in the poor range. These are screening bands, not machine guarantees. USP General Chapter <1174>, Powder Flow, describes several ways to assess flow, including compressibility, reinforcing that one measurement cannot describe every powder. Shape, particle size, and fines still matter.
A higher index may signal bridging or uneven feeding in a hopper. Consider a machine with a suitable outlet, controlled dosing, and adjustable agitation, then test the actual blend at realistic speeds. Test the real blend. I would not choose equipment from a single lab result; that shortcut is tempting, but it can miss changes caused by humidity or filling conditions. Keep the density method and test records with the machine trial.
Convert Production Demand into Required kg/h and Packs/min
Choosing a powder packaging machine starts with the production target, not the fastest number in a brochure. Calculate required kilograms per hour from the saleable product you need each shift. For example, 600 kilograms over six productive hours means 100 kg/h. Use actual running time, not the full shift length. Changeovers, cleaning, refills, and brief stoppages all consume time.
Then convert that mass rate into packs per minute. Divide the hourly output in kilograms by the net pack weight, then multiply by 1,000 and divide by 60. At 100 kg/h, a 500-gram pack requires about 3.3 packs per minute. A 100-gram pack requires about 16.7. Small packs can demand much faster, steadier dosing. Check whether the machine can sustain that pace with your powder, not just with an easy-flowing test material.
Powder behavior matters. Fine flour, instant drink mixes, and granular ingredients can differ in bulk density, dustiness, and flow. Ask for a trial using your own product and packaging. Record both average output and rejected or underweight packs. Real lines drift. A spreadsheet may look precise, but operators see clumps, settling, and hopper refills. Leave practical capacity headroom, perhaps 15–25%, after confirming the supplier’s test conditions. The estimate will still be imperfect; that is a reason to measure carefully, not to guess.
Match Auger or Cup Dosing to Bulk Density and Fill-Weight Tolerance
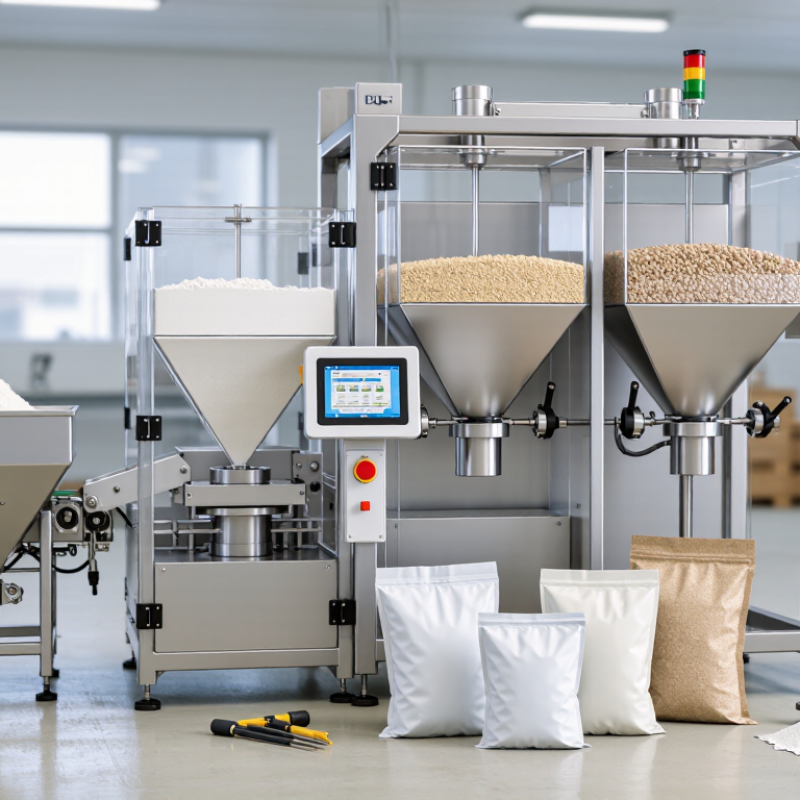
Bulk density is a practical starting point when choosing between auger and cup dosing. A light, cohesive powder may cling to hopper walls or form a bridge above the outlet. An auger moves material with a rotating screw, allowing adjustments to speed and dose settings. It often suits powders that need controlled feeding. Still, screw settings cannot fix every flow problem.
Free-flowing powders, such as some granular mixes, may work well with cup dosing. A cup measures a set volume, so changes in bulk density can change the delivered weight. Check the permitted fill-weight tolerance before choosing. If the range is narrow, test repeated fills on a calibrated scale. Compare results with a full hopper and a nearly empty one. The first trial may look consistent, then drift as powder settles. That detail is easy to miss.
Tips: Bring a representative powder sample for trials. Record fill weights, not just averages, and note dust, clumping, and residue around the dosing outlet. Recheck after changing batch or humidity conditions. A machine that runs smoothly in one test may need adjustment on the production floor.
Check Automatic Gravimetric Fillers Against OIML R 61
OIML R 61 is a useful reference when assessing automatic gravimetric fillers. It covers metrological requirements and testing for instruments that fill products by weight. Check which instrument type and accuracy class apply to your application. A supplier’s claim of compliance should be supported by test documentation, not just a brochure statement. Local rules may adopt the recommendation differently, so confirm the current requirements with the relevant authority.
Then test the machine with your actual powder. Fine flour, protein blends, and dusty additives can behave very differently in a hopper. Ask for trial results at your target fill weight and line speed. Review errors across repeated fills, not only the average. Watch for bridging, dust on the weighing area, and weight drift as the hopper empties. Small details matter.
A tidy test report is not the whole story. OIML-based testing helps assess weighing performance, but your production setup still matters. Changes in humidity or powder flow can affect results. I would also check how operators clean and recalibrate the machine between products. That part is easy to overlook. If possible, request records from trials using comparable materials, and clarify how performance is checked after installation.
Verify Food-Contact Materials Against EU 1935/2004 or Applicable FDA Rules
How to Choose the Right Powder Packaging Machine?
When comparing powder packaging machines, inspect every surface that may touch the product. This includes the hopper, auger, dosing tube, chute, seals, and internal coatings. A polished stainless-steel surface can look suitable, but appearance alone proves little. Check every surface.
For European use, verify that food-contact materials meet the relevant requirements of Regulation (EC) No 1935/2004, along with applicable material-specific rules and good manufacturing practices. For the United States, confirm compliance with FDA requirements applicable to the material and its intended conditions of use. Ask suppliers for material declarations, traceability records, and supporting test information. Details matter: powder composition, contact time, temperature, and cleaning methods can affect suitability. A generic certificate may not cover every component or operating condition.
Tips: List each product-contact part and request documentation for each one. Confirm that seals and coatings are included, not just metal parts. Match the evidence to your powder and cleaning routine. If a document is vague, ask for clarification before purchase. I have seen small parts overlooked during equipment reviews; it is an easy gap to miss. Keep the records with the machine’s technical file.
How to Choose the Right Powder Packaging Machine?
EU plastics overall migration limit: a useful reference when checking product-contact components.
Under EU Regulation 10/2011, the overall migration limit for plastic food-contact materials is generally 10 mg/dm², subject to specified test conditions and exceptions. Regulation (EC) No 1935/2004 provides the broader EU framework. In the United States, FDA requirements are material- and substance-specific; there is no single universal migration limit. Ask suppliers for declarations of compliance and supporting test documentation for every product-contact part, based on your intended foods and operating conditions.